We use cookles to Improve your online experience. By continuing browsing this website, we assume you agree our use of cookies.

Exploring the Realm of Printed Circuit Board Prototype Assembly
August 26th, 2025
124 views
Exploring the Realm of Printed Circuit Board Prototype Assembly
The realm of Printed Circuit Board (PCB) prototype assembly is a dynamic intersection of engineering precision, material science, and iterative problem-solving—far beyond the simple “build-to-design” process many assume. For hardware developers, startups, and electronics engineers, navigating this realm effectively means the difference between a prototype that validates ideas in weeks versus one that stalls projects for months. Industry data underscores this stakes: 58% of teams report spending 20+ hours troubleshooting prototype assembly issues (2025 IPC Prototype Development Report), often due to incomplete understanding of the realm’s technical nuances.
To truly explore this domain, we must dissect its core pillars: realm-specific PCB prototype design compatibility (ensuring designs fit assembly capabilities), precision-driven prototype assembly techniques (the craft of building reliable prototypes), iterative testing in PCB prototyping (validating performance across use cases), automated vs. manual PCB prototype assembly (choosing the right approach), and scalability-focused prototype assembly (designing for future production). Each pillar reveals critical technical insights that define successful prototype outcomes. This article explores these facets, draws on ShwayPCB’s expertise in navigating the realm, and provides actionable guidance to help you master PCB prototype assembly’s complexities.
Pillar 1: Realm-Specific PCB Prototype Design Compatibility
The first challenge in exploring PCB prototype assembly is ensuring your design speaks the “language” of assembly processes. realm-specific PCB prototype design compatibility isn’t just about meeting IPC standards—it’s about aligning every design choice with the physical constraints of SMT machines, reflow ovens, and inspection tools:
Key Compatibility Checks
- Component Package Alignment:
Not all component packages work in prototype assembly workflows. For example:
- 01005 passives, while compact, require specialized SMT nozzles (0.15mm) that only 30% of prototype facilities stock—opting for 0402 packages (compatible with 99% of SMT lines) eliminates delays.
- 0.3mm pitch BGAs demand X-Ray inspection for void detection, but many small prototype shops lack this equipment—0.4mm pitch BGAs balance density and accessibility.
ShwayPCB’s design compatibility tool flags incompatible packages upfront, saving teams 2–3 weeks of redesign—explore this at realm-specific PCB prototype design compatibility.
- Trace & Spacing for Etching Realities:
IPC-2221 Class 2 specifies 0.10mm minimum trace width/spacing for 1oz copper, but prototype fabrication adds variability:
- Chemical etching introduces ±0.02mm tolerance—designing with 0.12mm width/spacing (not 0.10mm) prevents short circuits caused by over-etching.
- For high-frequency signals (USB 3.0), trace spacing must be 2× the width (e.g., 0.24mm spacing for 0.12mm traces) to minimize crosstalk—this realm-specific rule isn’t always highlighted in basic design guides.
- Panelization for Prototype Efficiency:
Prototype panels differ from production panels—standard 120×150mm prototype panels maximize yield for small batches (e.g., 12 units of a 50×70mm PCB vs. 8 units in custom panels). Designing for these standard sizes reduces material waste from 30% to 5% and speeds up depaneling.
Pillar 2: Precision-Driven Prototype Assembly Techniques
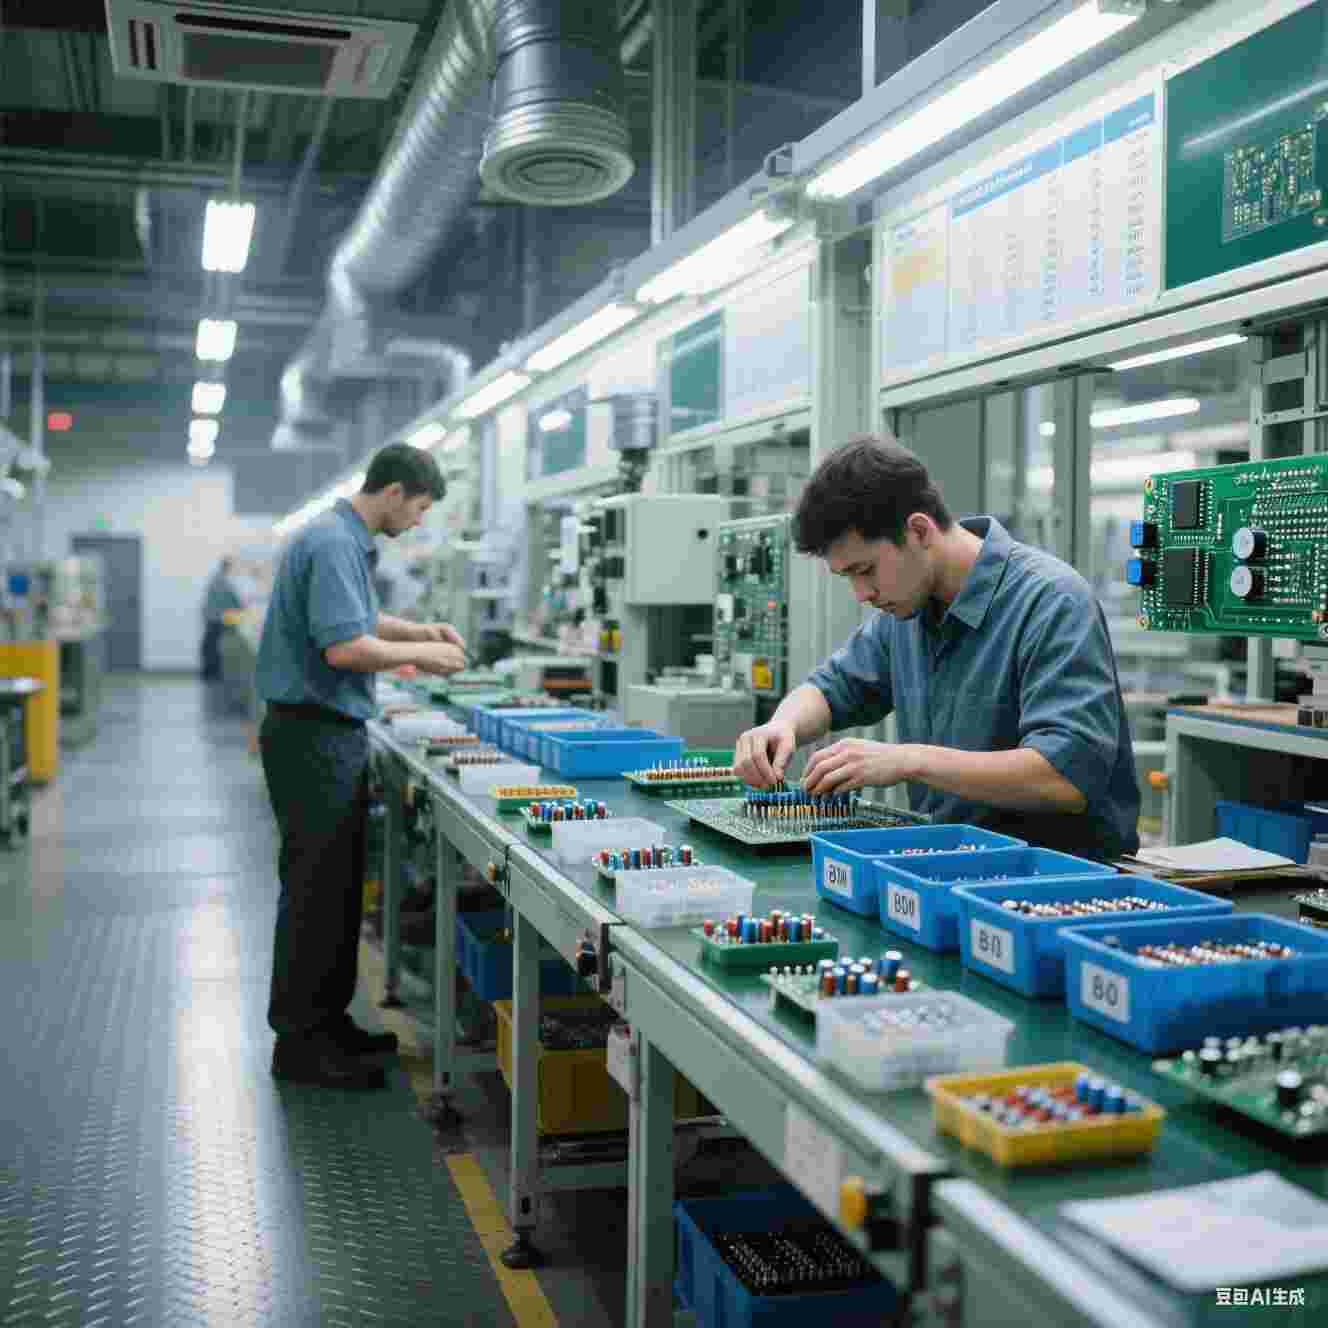
The heart of the PCB prototype assembly realm lies in techniques that balance speed with reliability—precision-driven prototype assembly techniques elevate prototypes from “functional” to “trustworthy” for validation:
Technical Techniques Unveiled
- Solder Paste Volume Calibration:
Prototype assembly demands exact paste volumes, as small batch sizes leave no room for error:
- 0402 resistors: 0.0045g paste per pad (not 0.003g) prevents tombstoning (22% of prototype defects).
- QFN packages: Laser-cut stencils with 0.12mm apertures (90% of pad size) ensure consistent solder coverage—avoiding cold joints in hidden thermal pads.
ShwayPCB uses automated paste inspection (API) to verify volume accuracy (±5%) before placement, reducing solder-related defects by 65%.
- Reflow Profiling for Prototype Components:
Prototype assemblies often mix heat-sensitive parts (e.g., LEDs) with high-temperature components (e.g., BGAs)—a one-size-fits-all reflow profile fails here. The solution is a “step-soak” profile:
- Pre-heat: 150°C for 60 seconds (gentle enough for LEDs).
- Soak: 180°C for 45 seconds (activates flux without burning).
- Reflow: 245°C peak for 10 seconds (solders BGAs without damaging LEDs).
This technique, tailored to the prototype’s component mix, achieves 98% first-pass yield (FPY) vs. 85% with generic profiles.
- Selective Soldering for PTH Components:
Through-hole (PTH) components in prototypes (e.g., USB-C connectors) require selective wave soldering, not manual soldering:
- Preheat temperature: 120°C (prevents thermal shock to the PCB).
- Solder wave height: 2mm (ensures full barrel filling without excess solder).
This precision reduces PTH joint defects from 18% to 2—learn more at precision-driven prototype assembly techniques.
Pillar 3: Iterative Testing in PCB Prototyping
Exploring the prototype assembly realm means embracing testing as an iterative process, not a one-time check. iterative testing in PCB prototyping uncovers flaws that surface only under real-world conditions, ensuring prototypes don’t fail during validation:
Iterative Testing Layers
- Electrical Validation (First Pass):
After assembly, automated probe stations test 100% of nets for:
- Continuity (≤1Ω resistance for signal paths).
- Isolation (≥10MΩ between adjacent nets).
This catches 40% of hidden defects (e.g., a cracked trace from handling) that visual inspection misses.
- Functional Testing (Second Pass):
Prototype-specific functional tests validate core features—for an IoT sensor prototype:
- BLE range testing (≥15m in open space).
- Power consumption (≤100μA in standby mode).
- Sensor accuracy (±0.5°C for temperature readings).
Failed tests trigger root-cause analysis (e.g., “range issue due to antenna trace impedance mismatch”)—not just scrapping the prototype.
- Environmental Stress Testing (Third Pass):
Prototypes that pass lab tests often fail in real environments—iterative environmental testing includes:
- Thermal cycling (-40°C to 85°C, 50 cycles) to identify solder joint fatigue.
- Humidity testing (85% RH, 85°C, 1000 hours) to check for corrosion.
A wearable prototype passed functional tests but failed thermal cycling—ShwayPCB’s iterative testing traced the issue to missing thermal vias under the MCU (fixed in 24 hours).
Explore this iterative approach at iterative testing in PCB prototyping.
Pillar 4: Automated vs. Manual PCB Prototype Assembly
A critical crossroads in the prototype assembly realm is choosing between automated and manual processes—automated vs. manual PCB prototype assembly each have distinct use cases, and the right choice depends on prototype complexity and volume:
Technical Comparison & Use Cases
|
Factor
|
Automated Assembly
|
Manual Assembly
|
Best For
|
|
Accuracy
|
±15μm (for 0.4mm BGAs)
|
±100μm (manual placement)
|
High-density designs (automated); 1–2 unit builds (manual)
|
|
Speed
|
1.5 hours for 100-component prototype
|
8 hours for 100-component prototype
|
Batches ≥10 units (automated); urgent 1-unit builds (manual)
|
|
Defect Rate
|
2–3% (FPY 97–98%)
|
8–12% (FPY 88–92%)
|
Reliability-critical prototypes (automated); low-stakes PoCs (manual)
|
|
Cost
|
\(1.80–\)2.20 per unit (10-unit batch)
|
\(5–\)8 per unit (1-unit batch)
|
Small batches (10–50 units: automated); single prototypes (manual)
|
ShwayPCB uses a hybrid approach: automated SMT for high-density components (BGAs, 0402 passives) and manual touch-up for PTH parts—combining accuracy and flexibility. Learn more at automated vs. manual PCB prototype assembly.
Pillar 5: Scalability-Focused Prototype Assembly
The most valuable prototypes in the assembly realm are those that scale seamlessly to production—scalability-focused prototype assembly ensures your prototype design doesn’t need a complete overhaul when moving to 100+ units:
Scalability Design Principles
- Component Standardization:
Avoid prototype-only components (e.g., a sensor with 500-unit MOQ) that aren’t feasible for production. Instead, select parts with:
- MOQ ≤50 (e.g., TI TPS7A4700 LDO, MOQ 10).
- 2+ pin-compatible suppliers (e.g., STM32L476 vs. Nordic nRF52840).
ShwayPCB’s component database flags non-scalable parts, saving teams 4–6 weeks of redesign.
- Process Alignment with Production:
Prototype assembly processes should mirror production:
- Use the same solder alloy (SAC305) and reflow profiles as mass production.
- Panelize prototypes to fit production panels (e.g., 24 units per 300×400mm production panel).
This alignment reduces production ramp-up time by 40%—a startup’s IoT prototype moved from 10-unit prototype to 200-unit production with 97% FPY, no design changes needed.
- Documentation for Scaling:
Scalable prototypes require detailed documentation:
- Solder paste volumes and reflow profiles.
- Component placement coordinates (aligned with production SMT machines).
- Test plans (reusable for production quality control).
Explore scalability strategies at scalability-focused prototype assembly.
ShwayPCB: Your Guide Through the PCB Prototype Assembly Realm
Navigating the complexities of PCB prototype assembly requires a partner with deep realm expertise. ShwayPCB’s approach integrates all 5 pillars:
- Design Compatibility: Free DFM reviews to align designs with assembly capabilities.
- Precision Techniques: Automated SMT, custom reflow profiles, and API for paste verification.
- Iterative Testing: Electrical, functional, and environmental testing as standard.
- Hybrid Assembly: Automated accuracy for critical components, manual flexibility for PTH parts.
- Scalability: Component standardization and production-aligned processes.
Result: 98.5% FPY for prototypes, with 0% scalability issues when moving to small-batch production.
FAQ: Exploring the Realm of PCB Prototype Assembly
1. What’s the most overlooked aspect of PCB prototype assembly for new teams?
Design compatibility with assembly processes—teams often focus on functionality but ignore:
- Component package availability (e.g., 01005 resistors that few shops can assemble).
- Trace spacing for etching tolerance (0.10mm vs. 0.12mm).
ShwayPCB’s compatibility tool fixes this—learn more via realm-specific PCB prototype design compatibility.
2. When should I choose automated vs. manual assembly for my prototype?
- Automated: For batches ≥10 units, high-density designs (0.4mm BGAs), or reliability-critical projects (e.g., medical devices).
- Manual: For 1–2 unit proof-of-concept (PoC) builds or urgent repairs (24-hour turnaround).
ShwayPCB recommends hybrid assembly for most prototypes—automated SMT + manual PTH.
3. How many iterative test passes does a “reliable” prototype need?
3 passes are minimum:
- Electrical (continuity/isolation).
- Functional (core feature validation).
- Environmental (thermal cycling/humidity).
Skipping environmental testing risks field failures—ShwayPCB includes this in all prototype services via iterative testing in PCB prototyping.
4. Can a prototype be “too precise” for its intended use?
Yes—over-engineering (e.g., 0.3mm pitch BGAs for a simple sensor) increases cost and assembly time without value. ShwayPCB’s engineers help balance precision with needs:
- Simple IoT sensors: 0402 components, 0.12mm traces, 0.4mm BGAs (if needed).
- AI edge modules: 0201 components, 0.10mm traces, 0.4mm BGAs.
5. How do I ensure my prototype scales to production without redesign?
Focus on 3 scalability steps:
- Use production-ready components (low MOQ, dual-source).
- Align prototype panelization with production panels.
- Document all assembly processes (reflow profiles, paste volumes).
ShwayPCB provides a “scalability report” with every prototype—verify via scalability-focused prototype assembly.
6. What’s the average lead time for exploring a complete prototype assembly (design to tested unit)?
Standard lead time is 3–5 days for 1–50 unit prototypes (2–4 layers):
- 1 day: Design compatibility review + DFM fixes.
- 2–3 days: Assembly (SMT + inspection).
- 1 day: Iterative testing + report.
Expedited 24–48 hour delivery is available for urgent projects.
Partner with ShwayPCB to Explore PCB Prototype Assembly
The realm of PCB prototype assembly is rich with technical nuances—but it doesn’t have to be overwhelming. ShwayPCB’s team of engineers guides you through every pillar, from design compatibility to scalability, ensuring your prototype is reliable, test-ready, and production-aligned. Whether you’re exploring your first PoC or refining a production-ready design, their expertise turns complexity into clarity.
To request a prototype quote, submit your design for a free compatibility review, or learn more about navigating the prototype assembly realm, contact ShwayPCB at yuan@shwaypcb.com.

Copyright © 2005-2025 ShwayPCB : PCB Fabrication and Assembly Manufacturer. All Rights Reserved. POWERED BY UEESHOP


Copyright © 2005-2025 ShwayPCB : PCB Fabrication and Assembly Manufacturer. All Rights Reserved. POWERED BY UEESHOP