We use cookles to Improve your online experience. By continuing browsing this website, we assume you agree our use of cookies.

3 Special Requirements for Medical Electronics Low Volume PCBA
August 18th, 2025
198 views
3 Special Requirements for Medical Electronics Low Volume PCBA
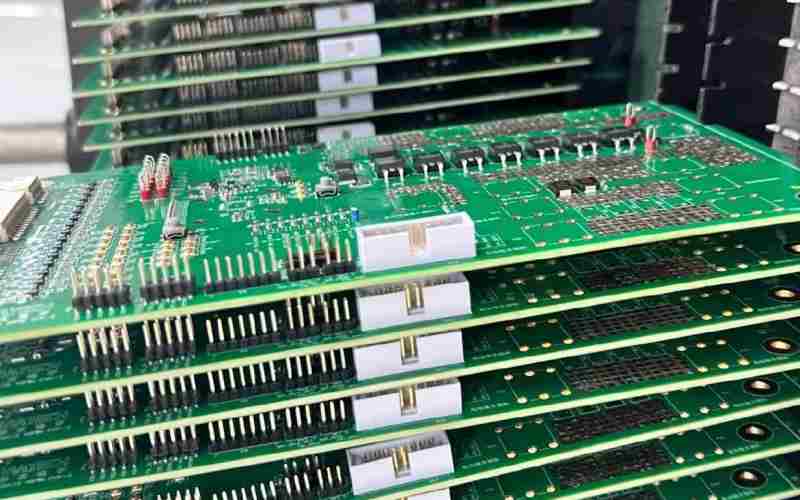
The safety and reliability of medical electronic devices are directly related to patients' lives and health, so their PCBA (Printed Circuit Board Assembly) production faces much stricter requirements than ordinary consumer electronics. For low-volume medical electronic PCBA (usually 10-500 units per batch), it is necessary to meet core requirements such as regulatory compliance and long-term reliability, while coping with the production characteristics of multiple varieties and short cycles. The production difficulty is significantly higher than that of mass-produced medical equipment or ordinary low-volume electronic products. This article will deeply analyze the 3 special requirements that low-volume medical electronic PCBA must meet, providing technical references for industry practitioners.
Requirement 1: Full-Process Compliance and Traceability
Medical electronic PCBA is subject to the world's strictest regulatory systems. Due to frequent line changes and process adjustments in low-volume production, a more refined compliance management system must be established to ensure that each product meets regulatory requirements.
1. Comprehensive Coverage of Regulatory Standards
- FDA and ISO 13485 Certification: This is the basic threshold for medical electronic PCBA production. ISO 13485 requires the establishment of a full-process quality system from design input to finished product delivery, including:
- Complete traceability of Design Verification (DV) and Design Qualification (DQ) documents
- Supplier management must pass the FDA QSR 820.50 standard audit
- CAPA (Corrective and Preventive Action) procedures must be implemented for production process deviations
- Special Requirements Corresponding to Product Classification:
- PCBA for Class III high-risk devices (such as defibrillators) must meet FDA PMA (Pre-Market Approval) requirements, and each batch must submit a process verification report
- PCBA for Class II devices (such as infusion pumps) must pass the Design History File (DHF) audit to prove the consistency of design and process
- Even custom medical equipment produced in small batches (such as special monitors for clinical trials) must retain a complete chain of evidence for regulatory compliance
2. Component-Level Traceability System
The traceability requirements for low-volume medical PCBA are far higher than those for ordinary electronic products:
- Batch-Level Traceability: All components must record the manufacturer, batch number, production date, and compliance certificates (such as FDA Device Master Record), and be bound to the PCBA serial number to achieve two-way traceability from components to finished products.
- Restricted Substance Control: It must comply with RoHS 2.0 medical exemption clauses (such as Annex IV allowing the use of lead solder in pacemakers), but the basis for exemption must be clearly stated in the product documentation.
- Long-Term Supply Guarantee: Medical-grade components (such as TI's medical-grade operational amplifier OPA211) should be selected, with a life cycle of usually ≥10 years, to avoid design changes due to component discontinuation, which is particularly important for low-volume long-term supply of spare part PCBA.
The compliance management of medical-grade PCBA is not a one-time certification but a continuous activity throughout the production cycle. For low-volume production, special attention must be paid to the recording and certification of process stability.
Requirement 2: Reliability Design and Verification in Extreme Environments
Medical electronic devices often work in complex scenarios such as humidity (e.g., operating rooms), vibration (e.g., portable devices), and electromagnetic interference (e.g., MRI environments). Their PCBA must pass rigorous reliability tests. Due to the limited sample size in low-volume production, the testing strategy must be more targeted.
1. Reliability Enhancement of Materials and Processes
- Substrate and Solder Selection:
- Prioritize high Tg FR-4 substrates (Tg≥180℃) to ensure no delamination during high-temperature sterilization (such as 134℃ steam sterilization)
- Solder must comply with ISO 10993 biocompatibility standards. For Class III device PCBA, it is recommended to use SAC305 lead-free solder (containing 3% silver to improve reliability)
- Connectors and other components with concentrated mechanical stress must use gold plating (thickness ≥30μin) to prevent poor contact due to plug-in fatigue
- Protection Process Upgrade:
- Moisture-sensitive components (MSL 3 and above) must be stored and soldered in an N2 environment to avoid reflow cracking caused by moisture absorption
- PCBA used in fluid environments (such as internal circuits of infusion pumps) must be coated with medical-grade conformal coating (such as Dow Corning 1-2577) and pass ISO 10993-5 cytotoxicity testing
2. Targeted Environmental Verification Testing
Low-volume medical PCBA must design test plans according to application scenarios:
- Accelerated Life Testing (ALT): Use temperature cycling (-40℃~85℃, 1000 cycles) and humidity testing (85℃/85%RH, 500 hours) to simulate 5 years of service life, with 10% of samples tested per batch (but at least 3 pieces).
- Functional Safety Verification:
- Power modules must pass EN 60601-1-2:2014 electromagnetic compatibility testing to ensure normal operation under 30V/m RF field strength
- Critical circuits (such as heart rate monitoring modules) must pass IEC 61010-1 overvoltage testing to verify fault tolerance under 2kV surge impact
- Clinical Scenario Simulation Testing:
- PCBA for portable devices must pass 1000 mechanical vibration tests (10-500Hz, 10g acceleration)
- PCBA for implantable devices must pass ISO 14708-1 sterility testing to verify packaging integrity
The reliability testing of medical device circuit assembly must cover both "normal use + single fault" scenarios. Although the test samples for low-volume production are small, they must include extreme condition verification.
Requirement 3: Cleanliness and Pollution Control
Pollution of medical electronic PCBA may cause equipment failure (such as short circuits) or patient infection (such as biocompatibility risks). Due to frequent line changes in low-volume production, cleanliness control must be more flexible and strict.
1. Graded Control of Production Environment Cleanliness
- Cleanroom Class:
- Class 8 (ISO 14644-1) cleanroom is the basic requirement, with the number of particles ≥0.5μm per cubic meter ≤352,000
- PCBA for implantable devices must be produced in a Class 7 cleanroom to reduce reliability risks caused by particle pollution
- Local areas (such as solder paste printing areas) must achieve Class 5 cleanliness through FFU (Fan Filter Unit) to control solder paste pollution
- Personnel and Material Control:
- Operators must wear sterile cleanroom clothing (covering to the neck, with sealed cuffs) and pass through an air shower (wind speed ≥20m/s) before entering the workshop
- Materials must undergo 3 layers of packaging stripping and UV disinfection (30 minutes, wavelength 254nm) before entering the cleanroom, and bare PCB boards must be stored in vacuum packaging
2. Types of Pollutants and Control Measures
- Chemical Pollution:
- Solder paste flux residues must be ≤25μg/cm² (detected by ion chromatography) to avoid corrosion or leakage risks
- Cleaning agents must use medical-grade isopropyl alcohol (purity ≥99.9%), and halogen-containing cleaners are prohibited (may produce toxic residues)
- Particle Pollution:
- Assembled PCBA must pass 100% visual inspection (20x magnifying glass) to ensure no free particles ≥50μm
- Test fixtures must use antistatic materials (surface resistance 10⁶-10⁹Ω) to avoid particle generation due to friction
The core of cleanroom PCBA production is to establish a pollution traceability mechanism. For low-volume production, it is necessary to record the production environment parameters (temperature, humidity, particle count) of each PCBA to facilitate later quality problem analysis.
FAQ: Common Questions About Low-Volume Medical PCBA
Q1: Why is the production cycle of low-volume medical PCBA 30%-50% longer than that of ordinary low-volume PCBA?
A: Medical electronic PCBA requires additional compliance activities, such as: first articles of each batch must pass full-item testing (2-3 days more than ordinary PCBA), component traceability document review (adding 1-2 days), and cleanroom line change cleaning (4 hours more than ordinary workshops). These links ensure compliance but extend the production cycle. The cycle management of medical device circuit assembly needs to balance compliance and efficiency.
Q2: How to balance cost and reliability testing requirements in low-volume production?
A: An "accelerated testing + statistical analysis" strategy can be adopted: ① The number of test samples per batch = 3 + √N (N is the batch size), which meets statistical confidence requirements and controls test costs; ② Use temperature cycling (-55℃~125℃) to accelerate aging, with 100 cycles equivalent to 1 year of use at room temperature; ③ Key test items (such as biocompatibility) can be entrusted to third-party laboratories to share costs using their equipment.
Q3: What is the difference between DFM for medical electronic PCBA and ordinary PCBA?
A: Medical electronics DFM needs to additionally consider: ① Redundant design (such as dual backup of key circuits) to meet IEC 61508 functional safety requirements; ② Cleanability design (such as component spacing ≥0.8mm to facilitate residue cleaning); ③ Maintainability (such as test point spacing ≥2.54mm to facilitate fault diagnosis). DFM for low-volume production needs to balance one-time cost and long-term reliability.
Q4: How to handle design changes for low-volume medical PCBA?
A: Design changes must implement FDA's Design Control process: ① Submit a change application (including change reasons and impact analysis); ② Conduct verification and confirmation (such as biocompatibility testing of new components); ③ Update DHF and DMR (Device Master Record); ④ Obtain approval from customers and regulatory authorities (if applicable). Even in low-volume production, unapproved design changes may lead to product recalls.
ShwayPCB: Professional Service Provider for Low-Volume Medical Electronic PCBA
ShwayPCB specializes in medical-grade PCBA production, with full-process capabilities to meet the special requirements of medical electronics:
- Possesses ISO 13485 certification and FDA registration qualifications, with Class 7 cleanroom (1500㎡) and Class 8 cleanroom (3000㎡) to flexibly meet the needs of different medical devices
- Establishes a dedicated library of medical components (including 5000+ medical-grade components) to achieve full-link traceability from procurement to production
- Provides dedicated DFM analysis for medical electronics, focusing on optimizing reliability and cleanability design, with a first-article pass rate ≥98%
Whether it is low-volume trial production of clinical trial equipment or long-term spare parts supply, we can ensure that PCBA meets medical regulations and performance requirements. For customized solutions, please contact yuan@shwaypcb.com.

Copyright © 2005-2025 ShwayPCB : PCB Fabrication and Assembly Manufacturer. All Rights Reserved. POWERED BY UEESHOP


Copyright © 2005-2025 ShwayPCB : PCB Fabrication and Assembly Manufacturer. All Rights Reserved. POWERED BY UEESHOP